 GEBHARDT Fördertechnik GmbH
GEBHARDT Pallet Conveyor Technology
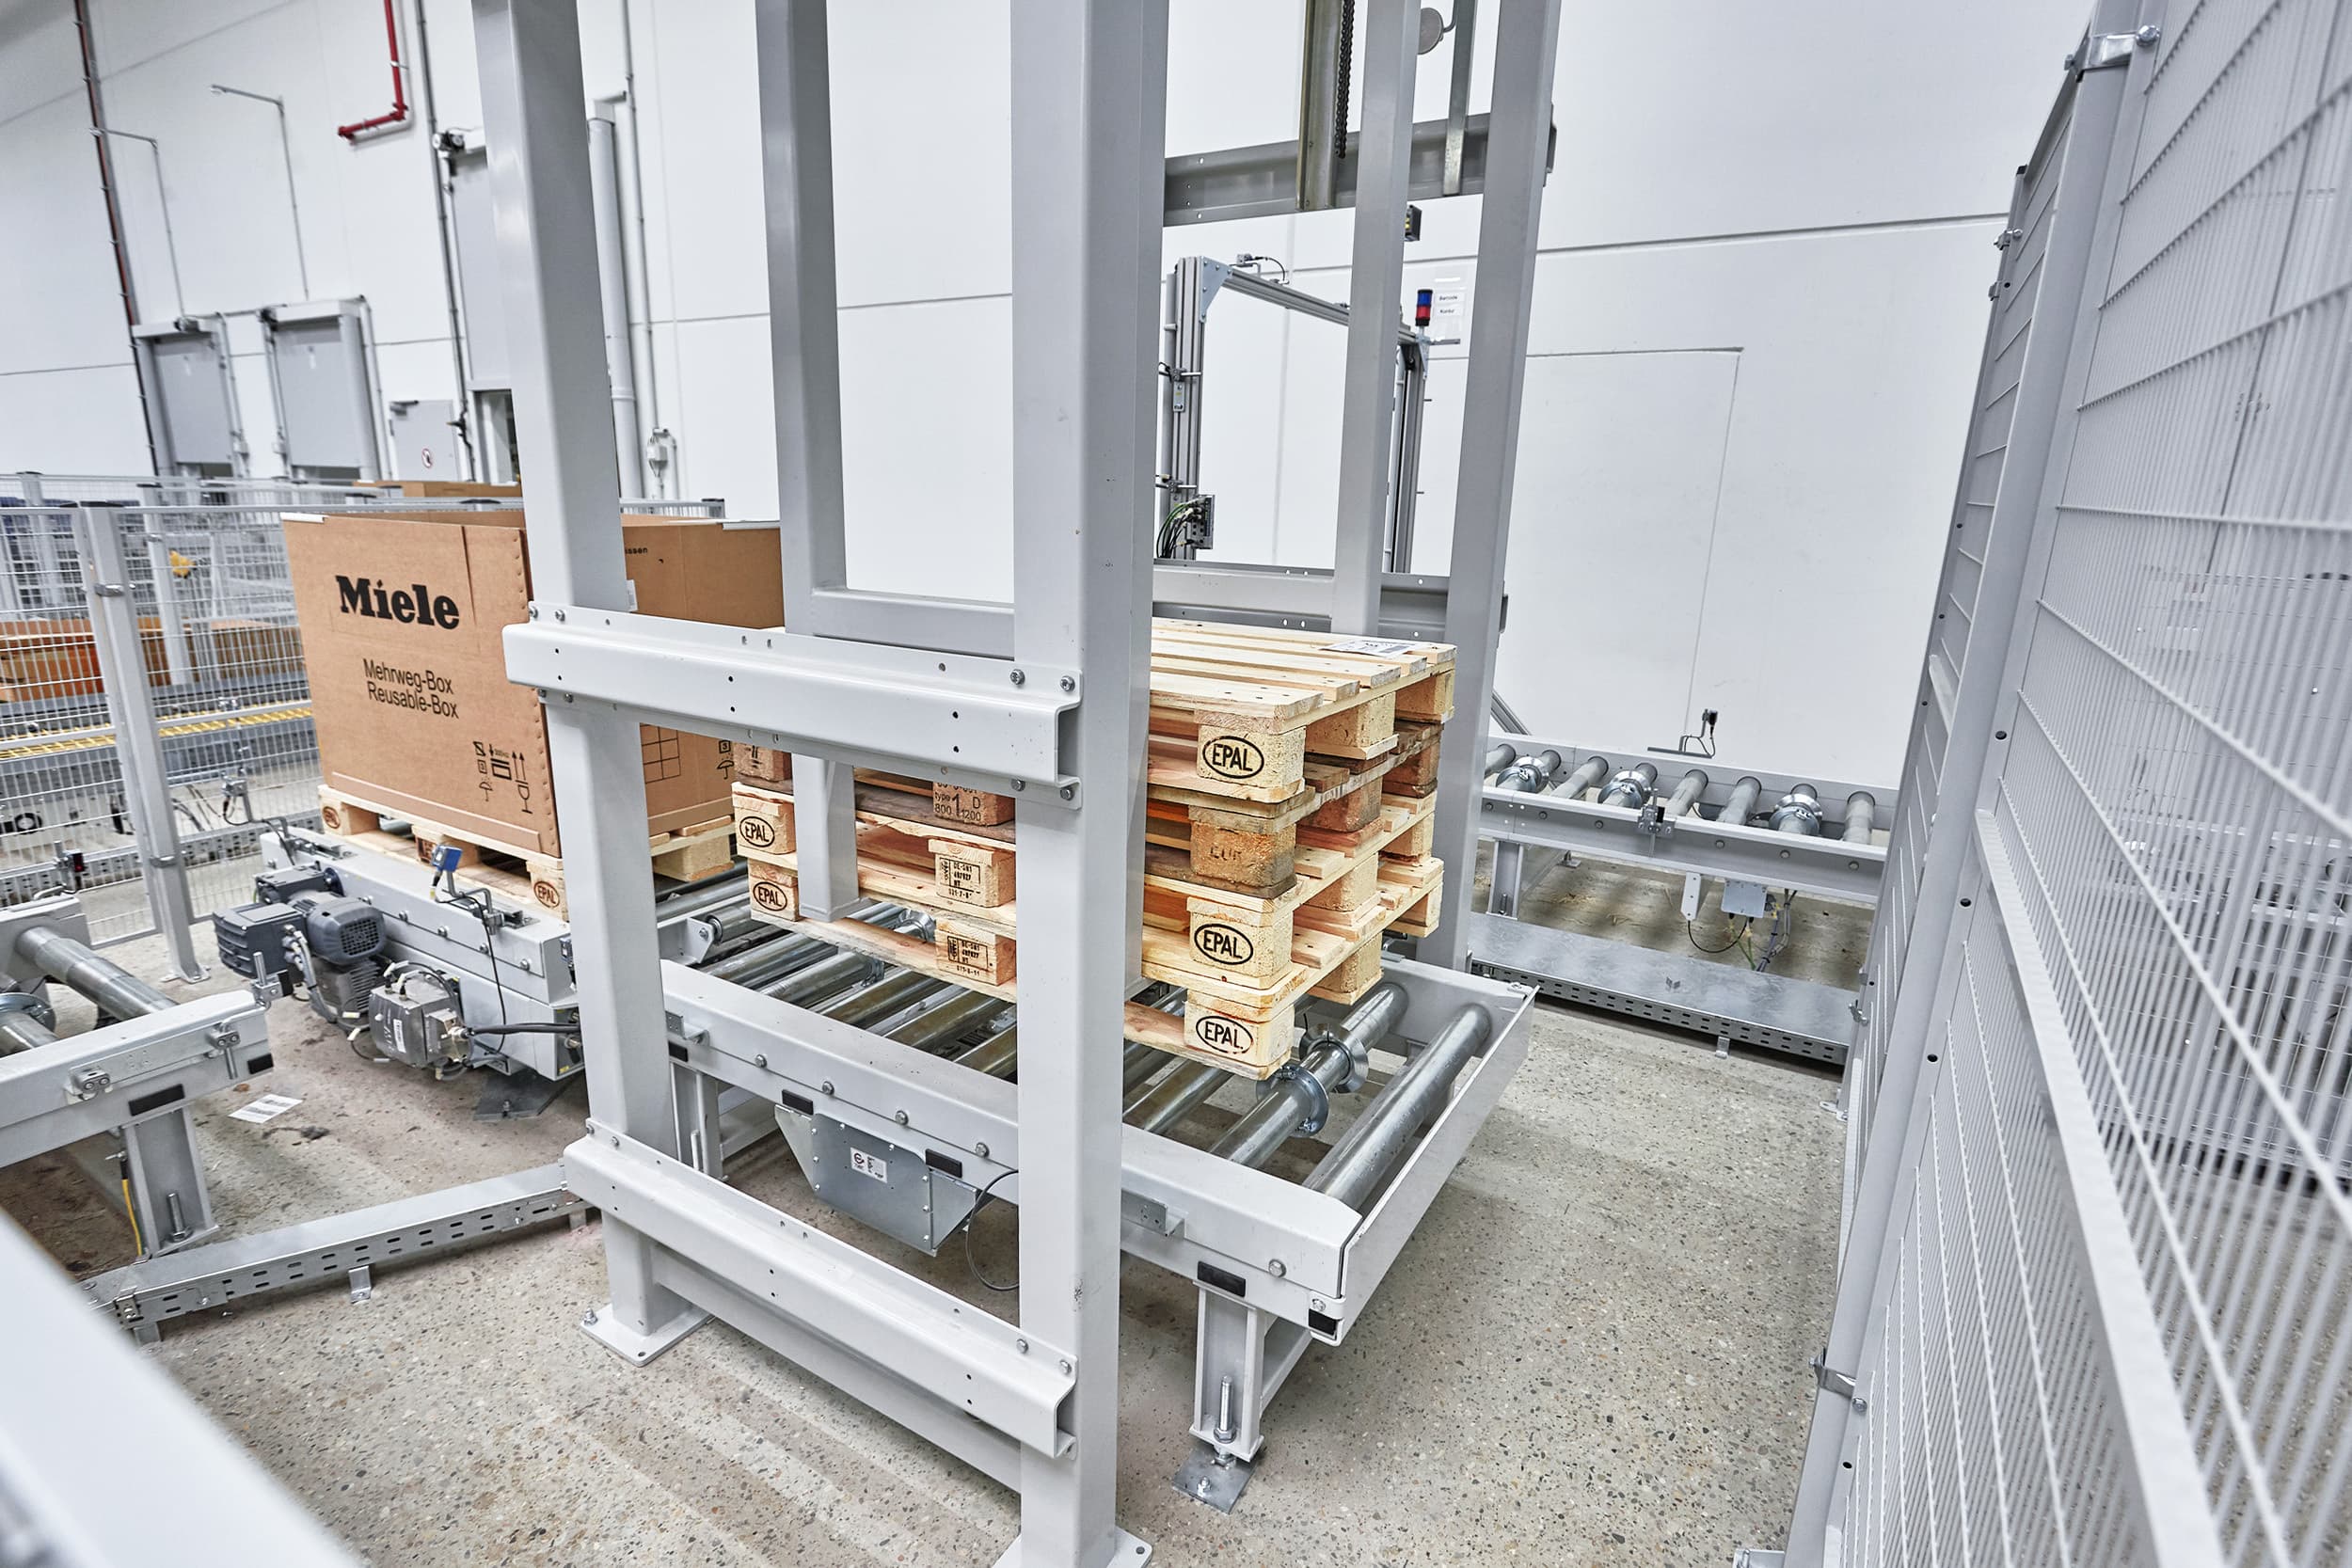
The GEBHARDT pallet conveyor system is a versatile Solution developed specifically for the requirements of modern conveyor systems. It offers optimized routing, efficient accumulation management, and precise lifting and rotating systems. Thanks to its seamless integration into existing intralogistics processes, the Solution maximizes efficiency while simultaneously reducing operating costs.
Overview
The GEBHARDT pallet conveyor system provides companies with a future-oriented Solution perfectly tailored to the requirements of modern conveyor systems. Optimized routing ensures smooth pallet transport, while efficient accumulation management maximizes space utilization and reduces energy consumption. Precise lifting and rotating systems offer maximum flexibility in pallet handling and enable individual positioning. The Solution integrates seamlessly into existing intralogistics processes, thereby increasing both the efficiency and the cost-effectiveness of the entire conveyor system.
Screenshots & videos
Key facts
Features
- Use case
- Roller conveyor, Timing belt conveyor
- Conveying direction
- Reversible
- Industry
- Automotive, E-Commerce, Retail, Food, Parcel logistics, Pharma, Production, Returns, Textiles and fashion
- Market segment
- Enterprise, Small business, Mid-market
- Temperature range
- Ambient (+14 °C to +21 °C), Fresh (+4 °C to +7 °C)
Soft Facts
- Soft Facts
- 24/7 Support
Features
- Payload
- 1500 Kilogramm pro Meter
All reviews0
No published reviews yet. Reviews go through a double opt-in before they appear here. Write a review now →
Related articles in the Infopoint